Level 2: Aware
A Level 2 plant scores between 200 and 399 on the Factory Excellence Index. It measures some losses and holds some routines, but the data arrives late, methods vary from line to line and many actions stay open.
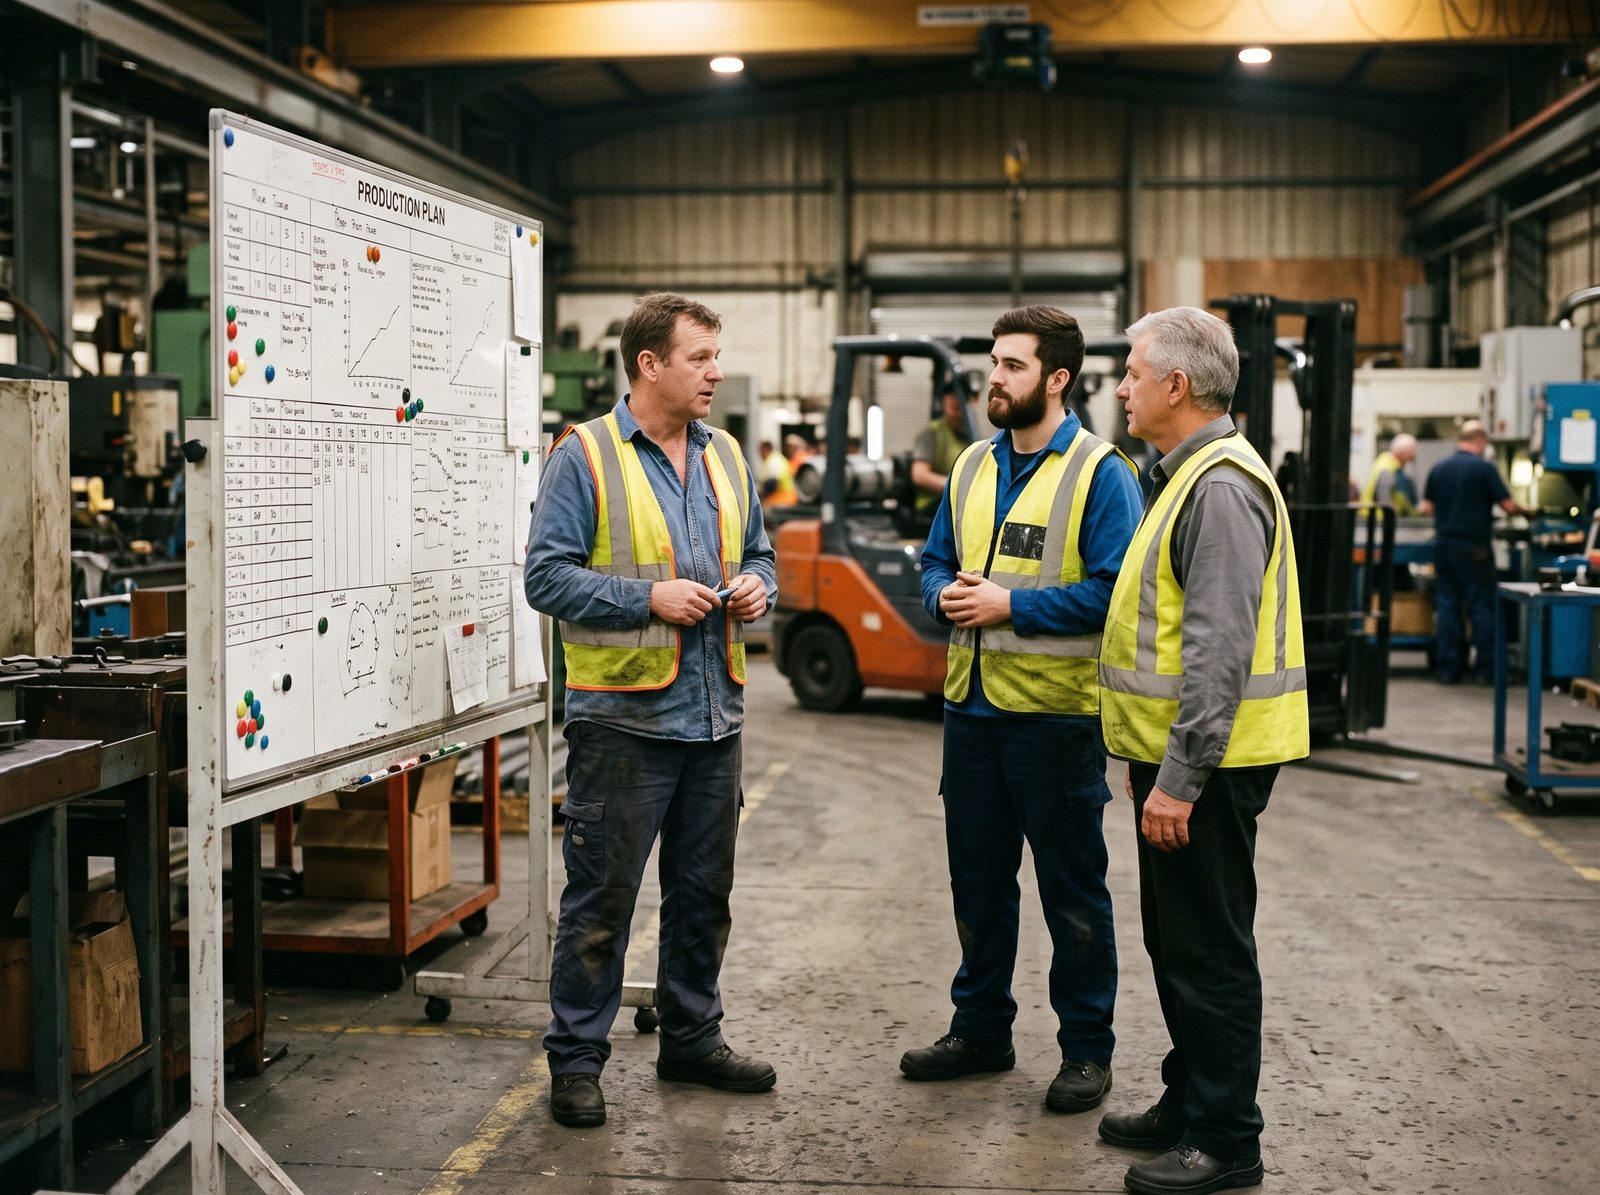
A 30-minute floor walk in a Level 2 plant
At shift change the outgoing team leader leaves a page of notes in a notebook by the line: 'gripper playing up again', 'short of labels', a figure crossed out. The incoming team leader reads them alone.
There is a board, and it was used recently. Output against plan is written for Monday and Tuesday; Wednesday is blank because the person who updates it was moved to another line. Operators rarely see a figure less than a day old.
The daily production meeting happens most days, but who attends and what is covered depends on who is in. Yesterday's figures come from paper sheets someone typed into a spreadsheet, and when the downtime figure looks bad, maintenance disputes it. The meeting ends with actions noted in the minutes, next to last week's actions that are still open.
During the walk the bottleneck stops. The operator knows whom to call and calls, but there is no rule for when to go to the next level if the technician does not come. The stop goes onto the paper sheet with a start time and the word 'maintenance'. The planned maintenance slot for this machine was pushed back last week to finish an urgent order.
A Level 2 plant has most of the parts of a system. What it lacks is timing and consistency: information arrives after the moment to act has passed, and each routine depends on who happens to be running it.
How the six pillars typically look at Level 2
The table follows the second anchored answer on each question of the model. Compare it with the pillar indices in your assessment report; the pillars page has the full anchors.
| Pillar | Typical practice at this level |
|---|---|
| Performance visibility | Operators fill in paper sheets per shift, typed into a spreadsheet later. The line learns it was behind the next day. An efficiency or OEE figure is quoted but calculated differently by line or shift. Output figures are accepted, downtime figures are questioned. |
| Daily management and shift routines | A daily production meeting with varying content and attendance. Handover by free-format notes. Boards updated irregularly. People know whom to call, with no time rules. Some supervisor routines exist but are not written down. |
| Loss and downtime problem-solving | Downtime totals reviewed monthly, with priorities set by experience. Causes found in informal discussion; countermeasures checked when someone remembers. Planned maintenance exists but is often postponed. Changeover duration is roughly known, short stops are not measured. |
| Improvement engine | Occasional projects or kaizen events not linked to targets. Actions recorded in minutes, many left open. Some written instructions, often out of date. Gains estimated by the project leader; many results slip back. |
| People and frontline ownership | Training records exist and team leaders get occasional training. Operators suggest ideas now and then, with little feedback. Informal thanks. An annual survey. |
| Data and connectivity foundations | A few local machine displays, or PLC data that is not collected. Ideal cycle times unknown or taken from the nameplate. Data moved to the ERP by hand and kept on shared drives. The IT policy applies but is not adapted to the shop floor. |
What keeps plants at Level 2
- Yesterday's data, last week's memory. Paper sheets typed in days later mean the meeting discusses stops nobody remembers clearly. The fix is not a better spreadsheet; it is capturing the reason during the shift.
- Two versions of every figure. When lines calculate efficiency differently and maintenance keeps its own downtime log, meetings spend their time on whose number is right. Until there is one definition and one official source, no loss can be prioritised with confidence.
- Actions that live in the minutes. An action written in a meeting record has nobody looking at it next week. The open list grows, and people learn that agreeing an action changes nothing.
- Projects with no target. Kaizen events not tied to a loss give the plant a good week and little after it. Without a link to a plant target, nobody notices when results slip back.
- Planned maintenance as the first thing to give. Each postponement looks reasonable on the day. Over months it turns planned work into breakdown work.
Five moves that take a plant to Level 3
Level 3 is where routines and definitions are written down and followed. These moves take the second 'next move' on the relevant questions of the model, in an order that builds one working weekly cycle.
- Month 1: fix the meetingWrite the agenda down, fix the attendance list and start on time every day for a full month, including days when the plant manager is away. At the same time, turn the handover notes into a one-page form with fixed fields: status, open issues, safety, quality, materials.
- Month 1: one definition, one reason listCompare how each line calculates its performance figure, agree one written definition with production, maintenance and finance (including what counts as planned time) and recalculate last month with it. Turn four weeks of free-text stop logs into 15 to 25 reason codes, entered during the shift. Keep the codes and ideal cycle times in one place.
- Month 2: the end-of-shift boardName one person per shift to write output against plan on the board at the end of the shift, with the two biggest reasons for any gap. The team leader explains the biggest loss to the next shift. An empty board becomes an item for the next morning's meeting.
- Month 2: a weekly Pareto and one methodBuild a weekly Pareto of stop time by reason for each main line and assign the top three items to named people. Pick one analysis method (5 Whys is enough to start), train supervisors on a real case from their own line and use it on every major event.
- Month 3: one action list and time rulesMove every action out of the minutes onto one shared list: what, who, by when. Review it at the same meeting every week and close or re-date every item. Add time rules to the escalation page, stating after how many minutes each level is called, and post it at the line.
Then take the assessment again. If the score has moved but the level has not, look at the pillar indices: the weakest-pillar rule may be the reason.
What Level 2 means for recognition
Level 2 plants are not eligible for Factory Excellence Recognition. They receive the full report, including the three biggest gaps with a 90-day move for each, which serves as the plan for the next quarter.
Recognition opens at Level 3, when a plant can request verification and be considered by its league jury.
The overall level cannot be more than one level above the weakest pillar's level. A plant can score 400 or more and still be shown at Level 2 because one pillar is at Level 1. The fastest route to Level 3 is then to lift that pillar, not to push the strong ones further. See the methodology.
Questions
Our score is above 400 but the report says Level 2. Why?
Because of the weakest-pillar rule: the overall level cannot be more than one level above the weakest pillar. If one pillar index is below 200, that pillar is at Level 1 and the overall level stops at Level 2. The report shows every pillar index, so the pillar setting the limit is easy to find.
Do we have to replace paper sheets with a system to reach Level 3?
No. The Level 3 answer on stop capture describes operators logging stops during the shift in a spreadsheet or terminal, choosing from a reason list. A shared spreadsheet on a line PC does the job. What matters is that the reason is chosen during the shift, not reconstructed afterwards.
Which pillar should we work on first?
Start with the three gaps your report lists. If you want a single place to begin, make the daily meeting run on time every day: it gives every other pillar somewhere to be reviewed.